 English
 русский
 عربى
Industry News
Home / News / Industry News / Seamless Stainless Steel Pipe Schedule: Wall Thickness Charts and How to Specify
A schedule names a wall thickness, not a pressure class — and on seamless stainless pipe it is the S series that decides the number you actually receive.
A drawing line reads DN50, SCH 40S, ASTM A312 TP316L, seamless. Three people read it three ways. Purchasing sees a weight per metre to price, the welder sees a wall to bevel, the engineer sees a pressure envelope. All three are asking the same question: how thick is the wall, and is that thickness right for the duty?
Start with the conclusion. A seamless stainless steel pipe schedule defines nominal wall thickness only. Outside diameter stays fixed across every schedule, the bore and the mass per metre move with the wall, and pressure capability has to be confirmed separately against the design code, the operating temperature and the corrosion allowance. Get the schedule right and you hold half an answer; treat it as a strength rating and you will eventually buy the wrong pipe.
Nominal size (NPS or DN), outside diameter, schedule, material specification and grade. Leave any one of them vague and the mill quotes something you did not intend. The four schedules below are the ones that appear on most stainless drawings, with wall values as published in ASME B36.19M.
| NPS | Outside diameter (mm) | SCH 5S | SCH 10S | SCH 40S | SCH 80S |
|---|---|---|---|---|---|
| 1/2 | 21.3 | 1.65 | 2.11 | 2.77 | 3.73 |
| 1 | 33.4 | 1.65 | 2.77 | 3.38 | 4.55 |
| 2 | 60.3 | 1.65 | 2.77 | 3.91 | 5.54 |
| 4 | 114.3 | 2.11 | 3.05 | 6.02 | 8.56 |
| 6 | 168.3 | 2.77 | 3.40 | 7.11 | 10.97 |
Read the 2-inch row closely. Stepping from SCH 10S to SCH 40S moves the wall from 2.77 mm to 3.91 mm and the mass from roughly 3.9 kg per metre to 5.4 kg per metre — about 28 percent more material for the same outside diameter. Note also that 5S and 10S are published across a very wide size range, while 40S and 80S cover a narrower band. At large diameters the S series runs out altogether, which is why heavy stainless lines are usually bought on an agreed minimum wall in millimetres rather than on a schedule.
The S stands for stainless. The series was written so that stainless pipe could be ordered to lighter walls than carbon steel at the same nominal size, wherever the pressure class and the corrosion allowance allowed it. At small sizes the two often coincide: a 2-inch SCH 40 carbon pipe and a 2-inch SCH 40S stainless pipe are both 3.91 mm on the wall.
They do not behave the same. Pressure capability comes from allowable stress at temperature, wall, outside diameter and the governing design code — not from the schedule number. Grades such as 304L and 316L lose allowable stress faster than carbon steel as temperature rises, and 316L drops below 304L in the creep range. A 40S line comfortable at 30 °C can be under-designed at 350 °C while every number on the drawing stays identical.
A schedule tells you the wall. The code, the temperature and the corrosion allowance tell you whether that wall survives.
Corrosion behaviour, pickling and passivation requirements sit on the same side of the calculation, and a closer look at the characteristics of stainless steel pipes is a useful reminder of how much of a stainless specification has nothing to do with wall thickness at all.
Where the medium attacks the steel, engineers add wall on top of the pressure calculation. That extra millimetre or two is almost never expressed as a schedule — it is written as a minimum wall, and it should be quoted that way.
Before approving a schedule, confirm the allowable stress at the design temperature, add the corrosion allowance, then convert the result into a minimum wall. Only after that step does the schedule number become a convenient label rather than a decision.
Nominal is not delivered. Cold-worked seamless stainless pipe is normally accepted with a minus wall tolerance, and the exact figure belongs to the purchase specification — for ASTM A312 seamless pipe it commonly sits around 12.5 percent. Apply that to the 2-inch SCH 40S example and the thinnest acceptable wall is roughly 3.42 mm, working out near 4.8 kg per metre instead of 5.44 kg.
That gap shows up in two places:
Estimating weight from a schedule is straightforward once the wall and the outside diameter are known.
Mass per metre in kilograms = 0.02466 × wall thickness × (outside diameter − wall thickness), with both dimensions in millimetres. For 2-inch SCH 40S: 0.02466 × 3.91 × (60.3 − 3.91) = 5.44 kg per metre.
Schedules were invented for piping systems — lines that carry fluid, join by welding or threading, and are rated by pressure class. A large share of the tube leaving a cold-rolling mill never becomes a line at all. It becomes a sleeve, a bushing, a guide rod, a tool housing or a spring seat, and for those parts the schedule tells a machinist almost nothing.
Machined parts are specified by outside diameter and inside diameter tolerance, wall eccentricity, straightness, cut length, surface condition and heat treatment. A 45 carbon steel seamless pipe ordered to a tight inside diameter machines very differently from the same nominal size bought to a piping schedule, even when the nominal wall is identical.
That difference is worth remembering at quotation stage. If the drawing shows a finished component, send the machining allowances instead of a schedule, and ask the mill to confirm the process route — cold rolling, cold drawing, annealing — because the route, not the schedule, governs dimensional behaviour. Suppliers that cold-roll tube for machinery customers, such as Zhejiang Qibin Steel Pipe Technology, work from those parameters rather than from pipe schedules.
Where a part carries load, the grade decides the outcome. Alloy grades such as 20Cr, 20CrMo and 40Cr are chosen for hardenability and for the strength reached after heat treatment, and high-strength 40Cr alloy seamless pipe for machinery is typically supplied as a blank that is quenched and tempered to reach its working properties. The schedule number plays no part in that decision, and neither does the pressure class of a piping standard.
Elastic parts sit even further from the schedule system. 60Si2Mn spring steel seamless pipe is selected for how it stores and returns energy under repeated load, which depends on chemistry, cleanliness and heat treatment rather than on a wall series. Ordering a spring seat, a torsion element or a shock absorber tube by schedule would be a category error, and the same logic applies to bearing steel tube, where hardness and wear resistance matter and a nominal wall series says nothing useful.
Five minutes of verification before the purchase order goes out prevents most of the expensive surprises later.
The costliest mistake on this list is copying a schedule from a carbon steel line onto stainless pipe of the same nominal size. The number looks familiar, the wall may even match, and the pressure capability still will not.
A schedule earns its place on a drawing because everyone in the chain recognises it. It stops being useful the moment the part is machined instead of piped, the temperature rises, or the medium eats steel. In those cases, put the wall, the tolerance and the grade into numbers, let the schedule ride along as a reference, and the pipe you receive will match the pipe you designed.

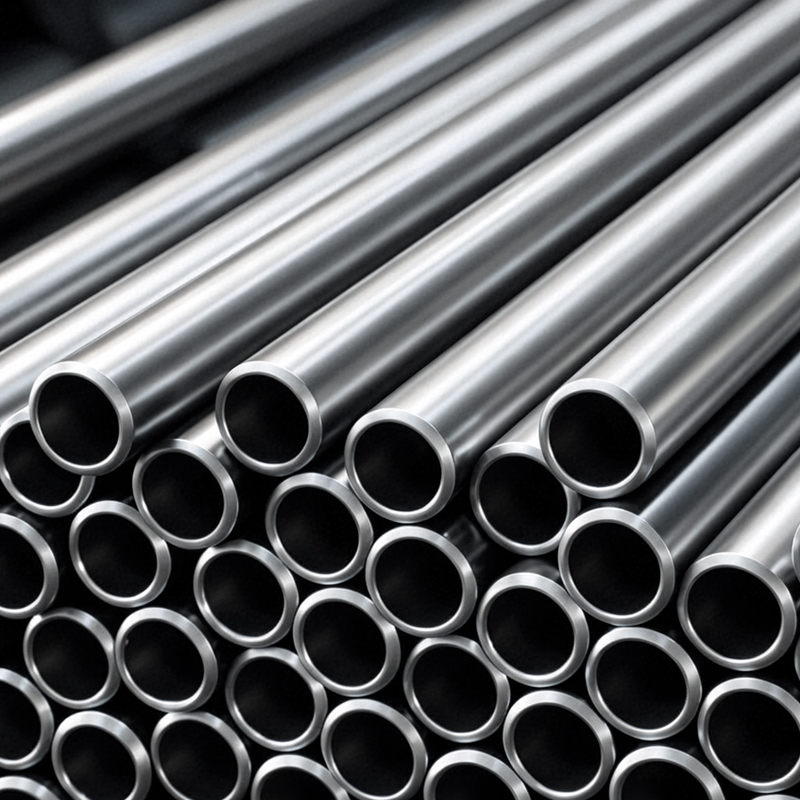
Seamless Piping Specification Seamless Stainless Steel Pipe Standards: A Buyer'...
Read MoreSeamless Pipe Engineering Seamless Stainless Steel Pipe Pressure Rating: Not a ...
Read MoreSeamless Stainless Steel Pipe Meaning: A One-Piece Tube Without a Weld What th...
Read MoreSteel Sourcing · Machining · Procurement Seamless Stainless Steel Pipe Dimensi...
Read More
 No. 8, Fengshan Road, Industrial Park, Mohuan Township, Longyou County, Quzhou City, Zhejiang Province, China.
 +86-18857033688
 postmaster@zj-qibin.com

